
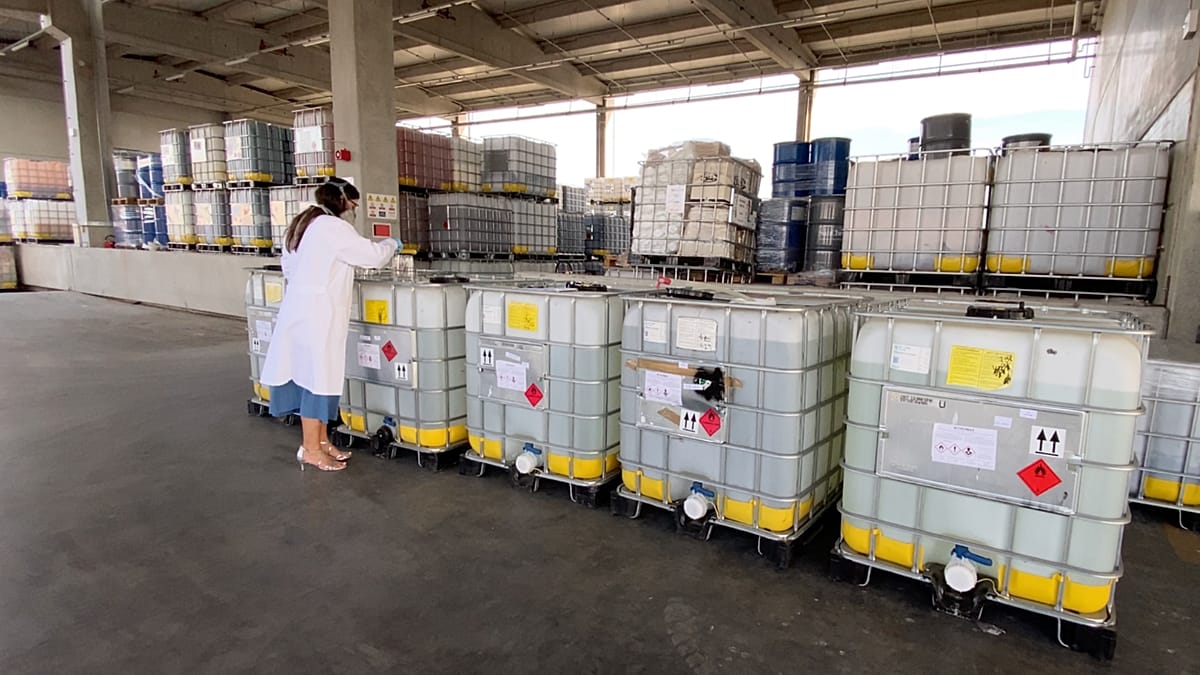



Equipped with air-filtering masks, workers at a recycling plant in Ivanić-Grad, Croatia, recycle ethanol, benzene or acetones, and thinners to dilute paints. These and other used solvents come from the food packaging, pharmaceutical or automotive industries. They are full of hazardous substances.
ADVERTISEMENT


ADVERTISEMENT
A complex process removes all their residues and turns contaminated solvents into clean ones, ready to be re-used.
“This is the contaminated solvent that we are taking from the machine and into the distillator. We are distilling it, and for the result we are getting the clean solvent that is used to further production. Clean as a whistle”, explains Mario Želježnjak, Production Supervisor at Premifab Ltd as he shows us the different technologies at an unassuming plant recently inaugurated.
Along with water and other impurities, the resulting waste is basically sludge that is used to produce energy that feeds the recycling facilities. “Everything is burned inside a rotary kiln and turned into harmless ash,” explains Mario. This ash can subsequently be used as a construction material.
Partially funded by the European Union, the clean-tech company claims to recycle around three million kilograms of used solvents annually—a 90% recycling rate for the contaminated raw material sent by its clients. Facing stiff competition from other major industry players in Germany, France, Spain, and Italy, the company must offer efficiency and versatility, explains its business development director, Igor Podravac.
“We have a lot of high demanding customers from pharmaceutical, automotive, paint industry,food packaging industry also. After they pollute a material and it is no longer usable for a second treatment, they send this material to us,” he explains while showing us the work done workers. “We are accepting the material, analysing the material, purifying the material and after all the parameters are checked, we return that material into the same production line to get a closed loop circular economy in real life.”
The first step starts at the company´s laboratory. Samples of used solvents are here first analysed to determine if and how they can safely and effectively be recycled. Very different parameters, including temperature, pressure or energy balance must be considered. “Maybe the distillation yield is too low, so it’s not really feasible, both material-wise and financial-wise. And on the other hand, if we have lots of distillation residue remaining, that we cannot do anything about it, we opt not to use that material at all,.”, explains Silvija Petković, Quality Control Director & Laboratory Manager. “The specificity within the solvents is their flammability. So they’re all flammable liquids, and we need to take all the precautionary measures in order not to burn anything, not to light anything up,” she adds.
After the distillation, and prior to sending the now clean solvents back to the clients, quality control checks are enforced again.
“This one does not conform because of the precipitation, so this one cannot go to the customer. So, this sample is going to stay here, and we need to do further filtration,” Silvija, explains to our camera while holding one sample. “This one is okay, no precipitation, whatsoever. It can be closed and sealed and put into the truck,”after checking a second, much transparent sample.
The approved recovered solvents are shipped to the clients in special containers. We follow one such delivery with Nikola Gojavić, a driver at the company. “This cargo is unique because it’s in a liquid state and is highly explosive. Great care is required during loading and transport, so specialised drivers are needed—it’s quite a challenging job,” he tells us while driving.
“The driver must be a specialist because, in the event of an accident or any incident, they must remain composed and be trained to carry out the necessary procedures.”
The cargo we follow brings back recovered solvents to a family business called Rotoplast. Each year, it manufactures approximately 5,000 tonnes of packaging and labelling for the food, energy and pet product industries. Solvents are used here to dissolve inks in the printing processes.
“It is important to us that our products, along with being highly effective from a production point of view, are also environmentally sustainable,” says Production Director Antun Čengić. “In cooperation with Premifab, we collect all our waste in a safe way, we transport it to their location, so that they can process it and return it to us as a new resource. With this, we reduce the costs of production.”
The company was founded in 1975 and currently employs 260 staff. Solvents are among the many recycled products that are reused here, claims the CEO, Blaženko Marić.
“80% of materials, it’s possible to use like this. We would like to move to mono materials. For all materials, for all customers. This is the plan for the next few years, to be completely phase out materials which are unrecyclable,” he explains.
Igor Podravac, its business development director, says their turnover has grown “approximately 20 to 25% per year” since they started operations, in December 2014. The company claims that, compared to primary production, recovered solvents generate up to 10 times less CO2 emissions.
Read the full article here